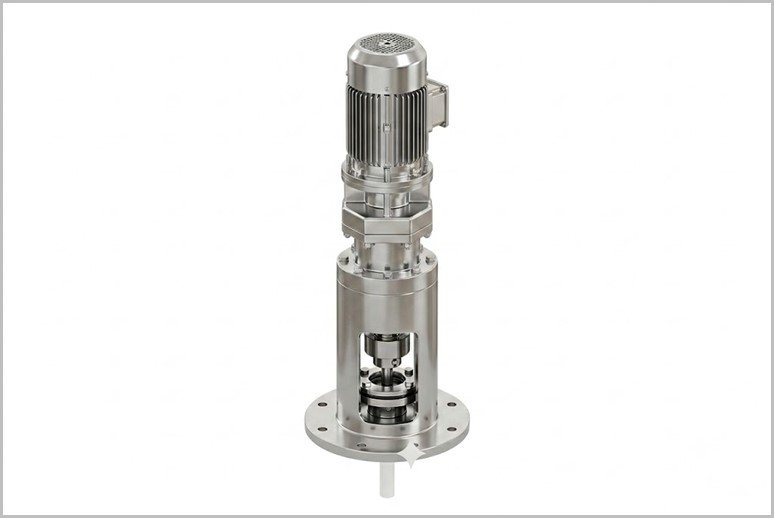
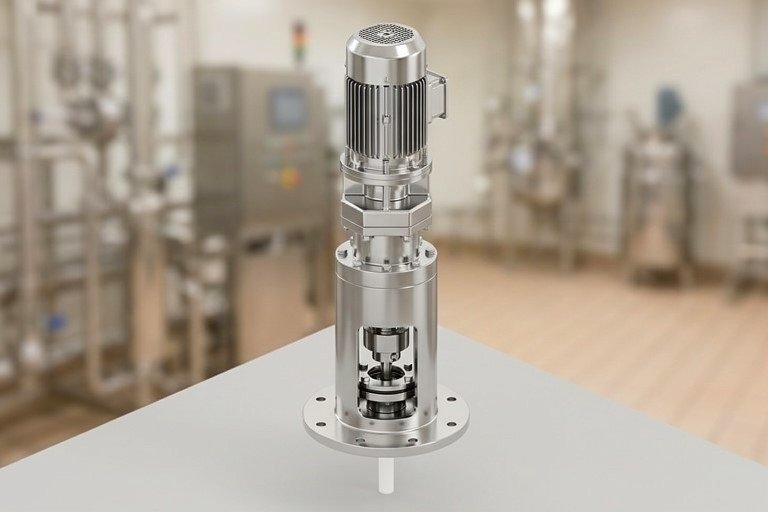
In the complex landscape of modern process engineering, achieving precise fluid dynamics is critical to product quality, reaction efficiency, and operational safety. At the heart of countless fluid processing systems sits the Chemical Agitator—often referred to as an industrial agitator or heavy-duty tank mixer. Manufactured by industry leaders like Adinath International, these mechanical devices are engineered to stir, blend, suspend, and homogenize fluids, viscous pastes, and multiphase mixtures within chemical reactors and storage vessels. This technical guide explores the core operational principles, critical functions, engineering classifications, and broad industrial applications of chemical agitators.
Industry Expertise and Quality Assurance
A typical chemical agitator consists of:
A Chemical Agitator (also called an industrial agitator or heavy-duty tank mixer) is a mechanical device engineered to stir, blend, suspend, and homogenize fluids, viscous pastes, and multiphase mixtures inside chemical reactors and storage vessels. It plays a central role in achieving precise fluid dynamics for product quality, reaction efficiency, and operational safety.
It efficiently processes liquids, solids, gases, and multi-phase systems. Custom impeller designs allow it to handle a wide range of viscosities and process requirements.
Chemical Agitators offer custom impeller options including axial, radial, turbine, anchor, and propeller designs. The choice depends on the specific mixing, blending, or suspension needs of the process.
They are built with corrosion-resistant materials such as SS 316, Hastelloy, and other exotic alloys. Hygienic/cGMP designs are available for pharmaceutical and food applications.
Top, side, or bottom entry configurations are available, allowing the agitator to be adapted to different tank designs and process layouts.
It ensures product uniformity and consistency, improves reaction rates and heat/mass transfer, supports low energy consumption with high pumping efficiency, and is fully customizable for specific viscosities and tank sizes.
They are widely applied in the Pharmaceutical, Nutraceutical, Herbal, Ayurvedic, Biotech, Cosmetic, and Chemical industries.
Yes. Variable speed control enables precise process adjustment, helping optimize mixing intensity, energy use, and batch reproducibility.
Yes. They are scalable from lab-scale units to large industrial tank sizes while maintaining robust construction for continuous heavy-duty operation and easy maintenance through accessible seals and drives.
By promoting efficient heat and mass transfer, delivering high pumping efficiency with low energy consumption, and providing durable, corrosion-resistant construction, they ensure maximum batch reproducibility, operational safety, and long-term reliability in demanding process environments.
Algeria | Angola | Argentina | Australia | Austria | Bahrain | Bangladesh | Belarus | Belgium | Bolivia | Botswana | Brazil | Bulgaria | Canada | Chile | China | Colombia | Costa Rica | Cuba | Czech Republic | Denmark | Dominican Republic | Ecuador | Egypt | El Salvador | Ethiopia | Finland | France | Germany | Ghana | Greece | Guatemala | Haiti | Honduras | Hong Kong | Hungary | India | Indonesia | Iran | Ireland | Israel | Italy | Ivory Coast | Japan | Jordan | Kazakhstan | Kenya | Kuwait | Lebanon | Libya | Malaysia | Mexico | Mongolia | Morocco | Mozambique | Myanmar | Netherlands | New Zealand | Nicaragua | Nigeria | Norway | Oman | Pakistan | Panama | Paraguay | Peru | Philippines | Poland | Portugal | Qatar | Romania | Russia | Saudi Arabia | Senegal | Slovakia | Singapore | South Africa | South Korea | South Sudan | Spain | Sri Lanka | Sweden | Switzerland | Taiwan | Tanzania | Thailand | Trinidad and Tobago | Tunisia | Turkey | Uganda | Ukraine | United Arab Emirates | United Kingdom | United States | Uruguay | Uzbekistan | Venezuela | Vietnam | Zambia | Zimbabwe
Connect with our engineering team to discuss your specific production requirements. We provide customized, cGMP-compliant machinery solutions designed to optimize your manufacturing facility and maximize output.
©Adinath International | Theme Developed By Pharma Machinery Manufacturer I Website updated on: 01 September 2026
WhatsApp us
