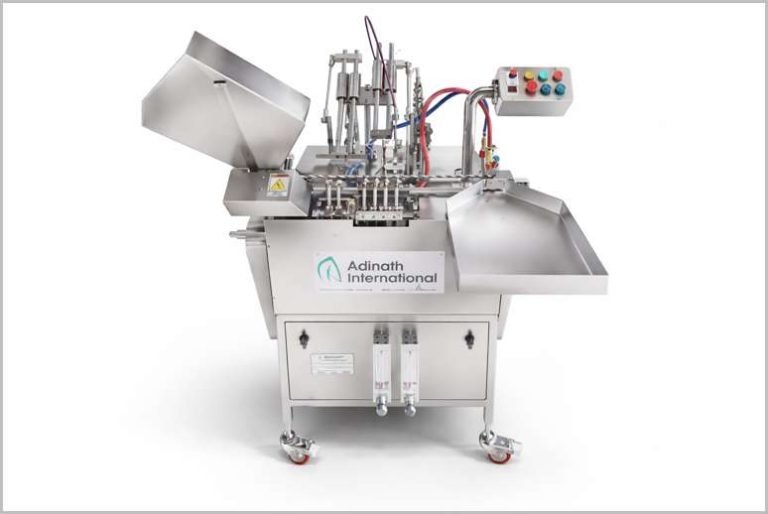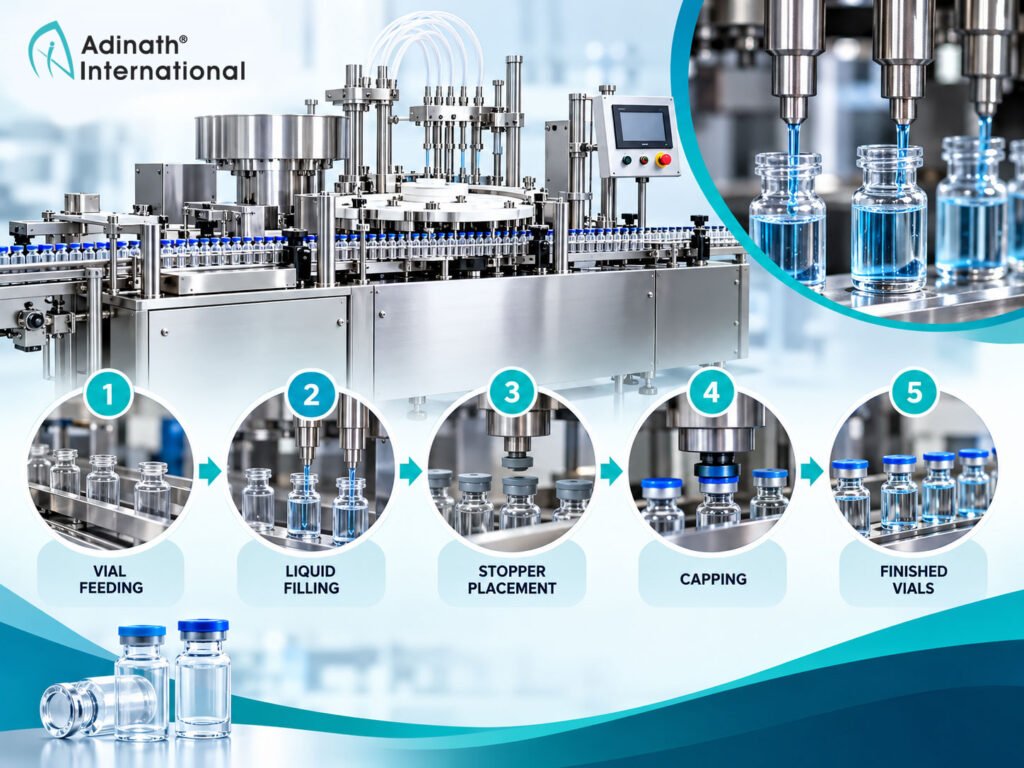
Vials are the most widely used containers for injectable products. A vial is a small glass or plastic bottle closed with a rubber stopper and secured with an aluminium or flip-off seal. Because the stopper can be pierced by a needle, vials are used for both single-dose and multi-dose products. Filling them accurately and closing them quickly is the job of the vial filling machine.
This guide explains the vial filling machine working principle for liquid products: how vials are fed and positioned, how the dose is measured and delivered, how rubber stoppers are placed, and how the filled vials are passed on for cap sealing. It is written for production engineers, maintenance teams and buyers who want a clear picture of what happens inside the machine. To compare machine types, you can see our vial filling machines.
What a vial filling machine does
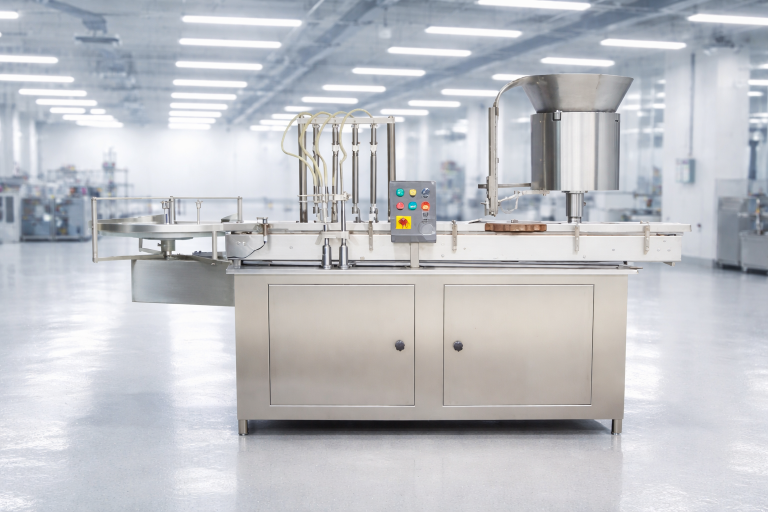
A liquid vial filling machine takes clean, sterilised empty vials, fills each one with a set volume of liquid through stainless steel nozzles, and closes it with a rubber stopper. On most production lines, the aluminium seal is then crimped on by a separate cap sealing machine placed directly after the filler. Some compact machines combine filling, stoppering and capping on one frame.
Machines differ in the number of filling heads, the vial sizes they handle, the dosing technology and the level of automation, but the working principle is the same. Our vial filling machine models show how these options are combined in practice. A “head” here means one filling position: one dosing pump with its nozzle. A four-head machine fills four vials at a time.
The vial filling process at a glance
| Stage | What happens | Why it matters |
|---|---|---|
| Infeed | Vials are fed from a turntable onto the conveyor | Steady supply without falls or jams |
| Positioning | Vials are stopped exactly under the nozzles | Nozzles must enter the neck cleanly |
| Dosing | A pump measures the set volume of liquid | Determines dose accuracy |
| Filling | Liquid flows through the nozzle into the vial | Controls foaming, splashing and drips |
| Stoppering | A rubber stopper is placed and pressed in | Closes the vial and protects the product |
| Outfeed to sealing | Vials move to the cap sealing machine | The stopper is secured with an aluminium seal |
Stage 1: Vial infeed
Vials arrive at the filler washed and sterilised. In a complete injectable line, they come from a vial washing machine and a sterilising or depyrogenation stage; you can browse all vial washing machines for the upstream equipment. On many fillers, vials are loaded onto a rotating infeed turntable, which gently guides them onto a stainless steel slat conveyor in a single row.
Side guides keep the vials upright and in line. Guides, star wheels and other parts that touch the vial are sized for each vial diameter, so a change of vial size means fitting the matching change parts and resetting the nozzle and stopper heights.
Stage 2: Positioning under the filling nozzles
To fill accurately, each vial must be stationary and centred under its nozzle. Machines achieve this in two main ways:
- Linear (in-line) machines let a group of vials, equal to the number of heads, run under the nozzles and hold them with stop gates or a positioning mechanism while filling takes place. The group is then released and the next group enters.
- Star wheel machines use a rotating star wheel with pockets that carries each vial to the filling position and holds it there during dosing.
Both approaches work on the same principle: the vial is fixed in position for the duration of the fill, then moved on to the stoppering station.
Stage 3: Dosing — how the volume is measured
The dosing system decides how much liquid goes into each vial. Two technologies are common on liquid vial fillers.
Piston (syringe) pumps
A piston pump is a precision cylinder with a plunger. On the suction stroke it draws a fixed volume of liquid from the product supply through an inlet valve; on the delivery stroke it pushes that volume out through an outlet valve to the nozzle. The volume is set by the stroke length, with a common adjustment for all heads and fine adjustment for each head. Piston pumps are volumetric and suit a wide range of liquids.
Peristaltic pumps
A peristaltic pump moves liquid by squeezing a flexible tube with rotating rollers. The product only touches the tubing, not the pump itself, which makes cleaning and product changeover simple: the tubing set can be replaced. The fill volume is controlled by how far the pump rotates for each fill. Tubing wears over time, so it is checked and replaced as part of routine maintenance.
Whichever dosing system is used, the fill volume is verified at start-up and at regular intervals by weighing filled vials, and adjustments are recorded.
Stage 4: Filling through the nozzles
The filling nozzles are lowered into the vial neck before liquid starts to flow. On many machines, the nozzles dive close to the bottom of the vial and rise as the liquid level rises. Filling from the bottom up reduces splashing and foaming, which is especially helpful for liquids that foam easily.
When the dose is complete, the nozzles withdraw. A drop left hanging on the nozzle tip can fall onto the vial neck or the conveyor, so machines use measures such as a short reverse movement of the pump at the end of the stroke (often called suck-back) and correctly sized nozzles to keep tips clean. A dry neck is also important for the stopper to seat properly.
On many automatic machines, sensors confirm that a vial is present before each head doses. This “no vial, no fill” function prevents liquid being dispensed onto the machine when a position is empty.
Stage 5: Rubber stoppering
Immediately after filling, each vial is closed with a rubber stopper. Stoppers are loaded in bulk into a vibratory bowl, which orients them so that they all face the same way and feeds them in a single line along a chute to the placement point.
Stoppers are then placed on the vials in one of two common ways. In a pick-and-place system, a mechanism picks a stopper from the chute and puts it on the vial. In a “pick-off” system, the moving vial collects the stopper from the end of the chute as it passes, and a pressing roller or plunger then pushes the stopper fully into the neck. Our vial filling and rubber stoppering machine combines both operations on one frame.
Most liquid products are fully stoppered. Partial stoppering, where the stopper is only half inserted, is used on lines where vials go on to freeze-drying; that process is outside the scope of this article.
Stage 6: Transfer to cap sealing
A rubber stopper on its own is not secure enough for storage and transport. After stoppering, vials move along the conveyor to a cap sealing machine, which places an aluminium or flip-off seal over the stopper and crimps it under the vial neck. In a line, the filler and the cap sealer are synchronised so that vials pass between them without manual handling. See the capping and sealing machines we manufacture for the sealing step.
Controls and synchronisation
All movements of the machine — conveyor, positioning, nozzle travel, pump strokes and stopper placement — follow a single cycle. On mechanically driven machines this is done with cams and a main drive; on many modern machines, a PLC with a touch-screen operator panel coordinates motors and sensors and lets the operator set fill volume, speed and counters. Interlocks stop the machine safely when a guard is opened or a fault is detected.
Output depends on the number of filling heads, the fill volume, the behaviour of the liquid (for example, how easily it foams) and the speed of the downstream cap sealer. The Automatic Vial Filling Machine range integrates infeed, filling and stoppering for continuous operation, while our Vial Liquid Filling Machine focuses on accurate liquid dosing.
Factors that affect fill accuracy
| Factor | Possible effect | What to check |
|---|---|---|
| Pump condition | Volume drift or variation between heads | Piston and valve wear; peristaltic tubing wear |
| Air in the product line | Low or variable fills | Priming, connections, product level in the supply |
| Liquid properties | Changes in delivered volume, foaming | Product temperature and viscosity; nozzle speed |
| Nozzle position and drips | Wet necks, poor stopper seating | Nozzle alignment, suck-back setting, nozzle condition |
| Vial positioning | Splashing, nozzle contact with the neck | Change parts, guide settings, star wheel timing |
| Stopper feeding | Missing or tilted stoppers | Bowl vibration, chute alignment, stopper condition |
Exact settings depend on the machine and the product. Always follow the machine manual and your validated process parameters.
Vial filling compared with ampoule filling
Ampoules and vials are both used for injectables, but they are closed in very different ways. An ampoule is sealed by melting its glass neck with a flame, so the filling machine includes burners and, often, gas flushing. A vial is closed with a rubber stopper and an aluminium seal, so the filling machine includes a stopper feeding system and works together with a cap sealer.
The filling machine in the complete vial line
A typical injectable vial line runs through vial washing, sterilising or depyrogenation, filling and stoppering, cap sealing, inspection and labelling. Each machine must match the output of the others, so the filler is normally selected as part of the line rather than on its own. Planning the line as a whole avoids bottlenecks and reduces manual handling between steps.
Conclusion
The vial filling machine working principle is a controlled sequence: feed and position a clean vial, measure the dose with a piston or peristaltic pump, fill through a diving nozzle without splashing or drips, place and press a rubber stopper, and pass the vial on for cap sealing. Fill accuracy depends mainly on the pump, the product supply and nozzle set-up, while reliable closure depends on a dry neck and consistent stopper feeding.
If you are choosing a vial filler or planning a complete line, our team can help you match the number of heads, vial sizes and dosing system to your product. Send an enquiry about a vial filling machine with your vial sizes, fill volumes and required output.